In the rigorous environments of food processing and pharmaceutical manufacturing, maintaining hygiene is not just a preference—it is a regulatory mandate. A washdown vfd (Variable Frequency Drive) is engineered specifically to operate in these challenging conditions, where equipment must be frequently cleaned with high-pressure water jets and aggressive chemical detergents. Unlike standard industrial drives, these specialized units eliminate the need for bulky, expensive external enclosures by integrating protection directly into the chassis.
The global shift toward automation in "wet" industries has accelerated the demand for robust motor control solutions that can withstand humidity, steam, and direct water contact. By implementing a washdown vfd, facility managers can significantly reduce downtime associated with electrical failures and moisture ingress, ensuring that production lines remain operational even during intensive sanitation cycles.
Understanding the nuances of washdown-rated technology is critical for optimizing Total Cost of Ownership (TCO). From energy efficiency to the reduction of stainless steel cabinet costs, the integration of these drives allows for a leaner, more hygienic plant layout. This guide explores how the right drive selection impacts operational reliability and safety in the most demanding industrial washdown environments.
The Technical Foundation of Washdown VFDs
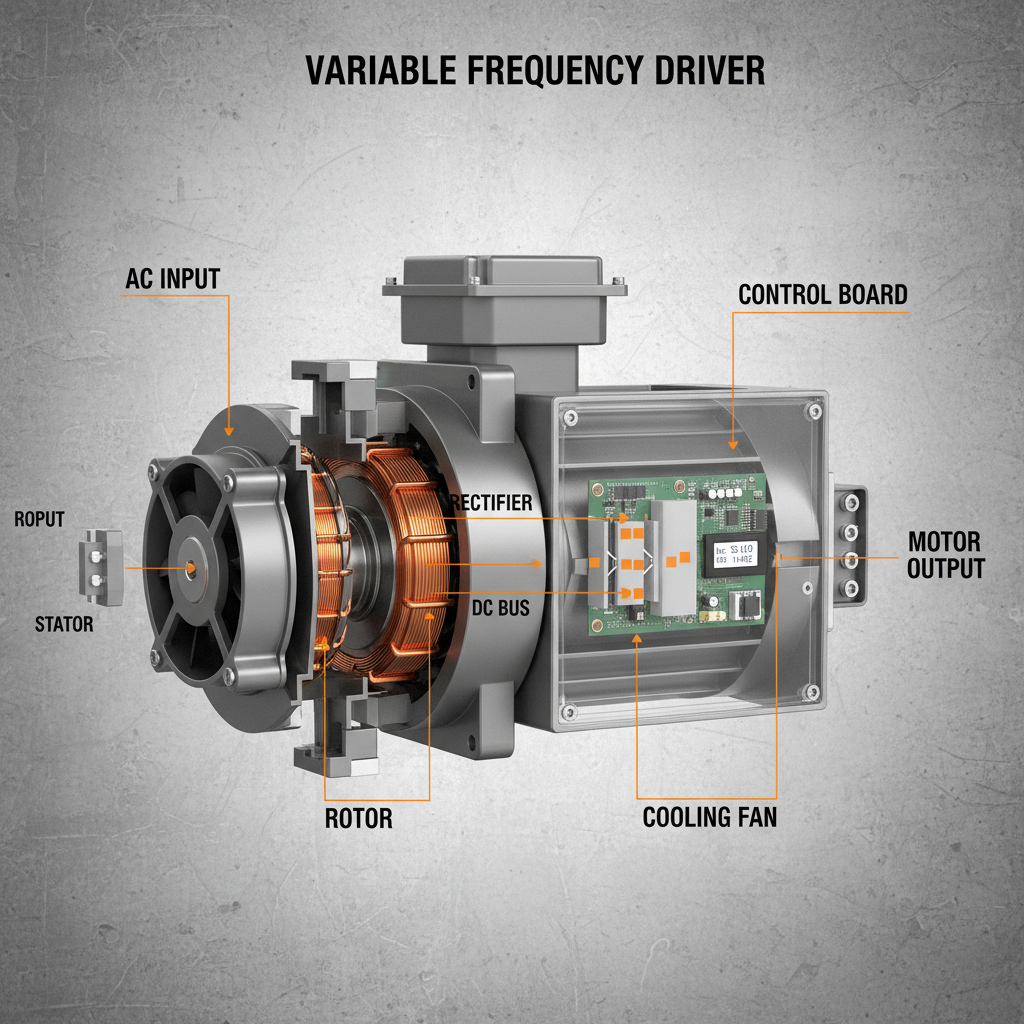
At its core, a washdown vfd is a motor controller designed with a sealed housing that prevents the ingress of liquids and particulates. While a standard VFD relies on airflow for cooling—which would invite moisture and contaminants into the electronics—washdown versions often utilize heat sinks or specialized thermal management systems that allow the unit to remain completely sealed while dissipating heat.
This engineering shift allows the drive to be mounted directly on the machine frame, closer to the motor. This "distributed" architecture reduces the amount of cabling required and eliminates the need for large, centralized electrical rooms, which are often difficult to keep clean and cool in food-grade facilities.
Industry Standards and IP Ratings for Wet Environments
When selecting a washdown vfd, the IP (Ingress Protection) rating is the most critical metric. For most washdown applications, an IP66 or IP69K rating is required. IP66 ensures protection against powerful water jets, while IP69K is the gold standard, indicating the device can withstand high-pressure, high-temperature washdowns, which are common in meat and dairy processing where steam is used to sterilize surfaces.
Beyond IP ratings, the material composition of the enclosure plays a vital role. Standard plastics may degrade when exposed to caustic cleaning agents like sodium hydroxide or peracetic acid. Therefore, high-grade stainless steel or specialized reinforced polymers are used to ensure the chassis does not corrode or crack over years of chemical exposure.
These standards are not merely suggestions but are often tied to ISO and FDA compliance. Failure to use a properly rated drive can lead to "arc flashes" or short circuits when water penetrates the housing, creating a significant safety hazard for plant operators and risking costly production halts.
Core Components and Engineering Durability
The durability of a washdown vfd begins with its sealing gaskets. These gaskets are typically made from Viton or high-grade silicone, materials chosen for their ability to maintain a tight seal despite the extreme temperature fluctuations encountered during a "hot wash" cycle followed by a "cold rinse."
The internal circuitry is often treated with a conformal coating. This thin polymeric film acts as a secondary line of defense; if a seal were to fail slightly, the coating prevents moisture from causing a short circuit on the PCB, thereby extending the lifespan of the washdown vfd significantly compared to uncoated alternatives.
Finally, the human-machine interface (HMI) is redesigned for these environments. Keypads are replaced by membrane switches or fully sealed touchscreens, ensuring that the operator can adjust parameters without allowing water to seep into the control board, maintaining the integrity of the overall system.
Performance Comparison of Washdown Control Methods
Depending on the application, engineers may choose between different implementation methods for their washdown vfd. Some prefer the "Fully Encapsulated" approach for maximum protection, while others use "Hybrid-Sealed" units for better thermal performance in high-ambient temperature zones.
Choosing the right method depends on the frequency of washdowns and the chemicals used. A facility that cleans every hour requires a more robust solution than one that cleans once per shift. The following chart illustrates the relative efficiency and durability ratings of various washdown implementation strategies.
Washdown VFD Implementation Effectiveness
Global Applications in Food and Pharma
Across North America and Europe, the adoption of washdown vfd technology is most prominent in the dairy and beverage sectors. In these regions, stringent HACCP (Hazard Analysis and Critical Control Points) guidelines mandate the removal of all organic residues, necessitating high-pressure cleaning. By using these drives, plants can automate conveyor belts and pumps without risking electrical failure during the cleaning phase.
In emerging markets in Southeast Asia, the shift toward modernized food processing is driving the installation of washdown-rated equipment. In remote industrial zones where technical support may be limited, the inherent reliability and lower maintenance needs of a washdown vfd make it a preferred choice over standard drives that require frequent replacement due to corrosion.
Long-Term Economic and Operational Value
The initial investment in a washdown vfd is typically higher than that of a general-purpose drive. However, the long-term value is found in the elimination of NEMA 4X stainless steel enclosures. A single high-quality stainless enclosure can cost more than the drive itself; by using a washdown-rated drive, this expense is removed from the bill of materials.
Operationally, the benefits manifest as reduced downtime. In a typical food plant, an unplanned motor controller failure can stop an entire production line, costing thousands of dollars per hour in lost throughput. The ruggedized nature of these drives minimizes these "nuisance trips" and hardware failures.
Furthermore, the energy efficiency provided by VFD technology—reducing motor speed to match actual demand—combines with the durability of washdown engineering to create a sustainable model. This reduces the carbon footprint of the facility while ensuring the highest levels of product safety and hygiene.
Future Innovations in Hygienic Automation
The next generation of washdown vfd systems is moving toward "Smart Hygienic Control." We are seeing the integration of IoT sensors that can monitor the internal humidity and temperature of the drive in real-time. If a seal begins to degrade, the system can alert maintenance before a failure occurs, moving from reactive to predictive maintenance.
Digital transformation is also introducing wireless parameterization. Since opening a sealed drive to change a setting risks introducing moisture, new drives allow engineers to adjust speeds and ramps via a secure Bluetooth or Wi-Fi connection from a tablet, keeping the washdown vfd completely sealed during operation.
Sustainability is also driving the use of biodegradable polymers for enclosures and more efficient Gallium Nitride (GaN) semiconductors, which generate less heat. This allows for even smaller, more compact washdown drives that don't require massive heat sinks, further optimizing the footprint of the industrial automation equipment.
Technical Specifications Comparison of Washdown VFD Solutions
| Protection Level |
Enclosure Material |
Thermal Management |
Suitability Score |
| IP66 |
Polycarbonate |
Passive Cooling |
7/10 |
| IP69K |
316 Stainless Steel |
Advanced Heat Sink |
10/10 |
| IP55 (Enclosed) |
Powder-coated Steel |
Forced Air/Fan |
4/10 |
| IP67 |
ABS Plastic |
Passive Cooling |
6/10 |
| IP69K |
Reinforced Polymer |
Composite Cooling |
9/10 |
| Custom Sealed |
Aluminum Alloy |
Liquid Cooled |
8/10 |
FAQS
IP66 provides protection against high-pressure water jets from any direction. However, IP69K is a more rigorous standard that includes protection against high-pressure (up to 1450 psi) and high-temperature (80°C) water, which is essential for steam-cleaning processes. For most industrial food washdown environments, IP69K is the recommended choice to ensure long-term reliability.
In most cases, no. One of the primary advantages of a washdown vfd is that it is designed to be mounted directly on the machine. This eliminates the need for an expensive NEMA 4X or IP66 stainless steel enclosure, reducing both the initial capital expenditure and the physical footprint of the installation.
Since fans would require vents (which let in water), washdown VFDs use passive thermal management. They are typically constructed with large external heat sinks or the enclosure itself acts as a heat radiator. The heat is transferred from the internal components to the outer shell via thermal conductive pads, allowing the unit to stay cool while remaining airtight.
Standard plastics can crack or discolor when exposed to caustic chemicals. However, professional washdown vfd units use 316 stainless steel or chemically resistant polymers designed specifically to withstand the pH levels of industrial cleaning agents, ensuring the structural integrity of the drive is maintained.
While these drives are built for longevity, it is best practice to inspect gaskets and cable glands every 6 to 12 months. Look for signs of "dry rot," cracking, or compression set in the rubber components. Replacing a seal proactively is significantly cheaper than replacing a drive that has suffered water ingress due to a worn gasket.
Yes, they are compatible with standard AC motors. However, for a complete "washdown system," it is recommended to pair the washdown vfd with a washdown-rated motor (IP66/69K). This ensures that the entire power train—from the controller to the motor—is protected against water and chemicals.
Conclusion
The implementation of a washdown vfd represents a critical intersection of electrical engineering and hygienic design. By prioritizing IP69K ratings, chemically resistant materials, and passive thermal management, these drives solve the age-old conflict between the need for precise motor control and the requirement for aggressive sanitation. The resulting increase in uptime, coupled with the reduction in enclosure costs, provides a clear economic advantage for any facility operating in a wet environment.
As the industry moves toward Industry 4.0, the integration of predictive diagnostics and wireless control will make these systems even more resilient. For plant managers and engineers, the transition to specialized washdown hardware is no longer an optional upgrade but a fundamental requirement for maintaining safety, compliance, and operational efficiency in a competitive global market. Visit our website for more professional automation solutions: www.tianjinyongkai.com